

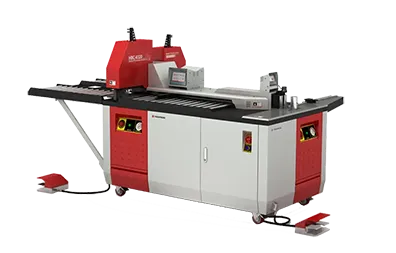
What Is Busbar Bending?
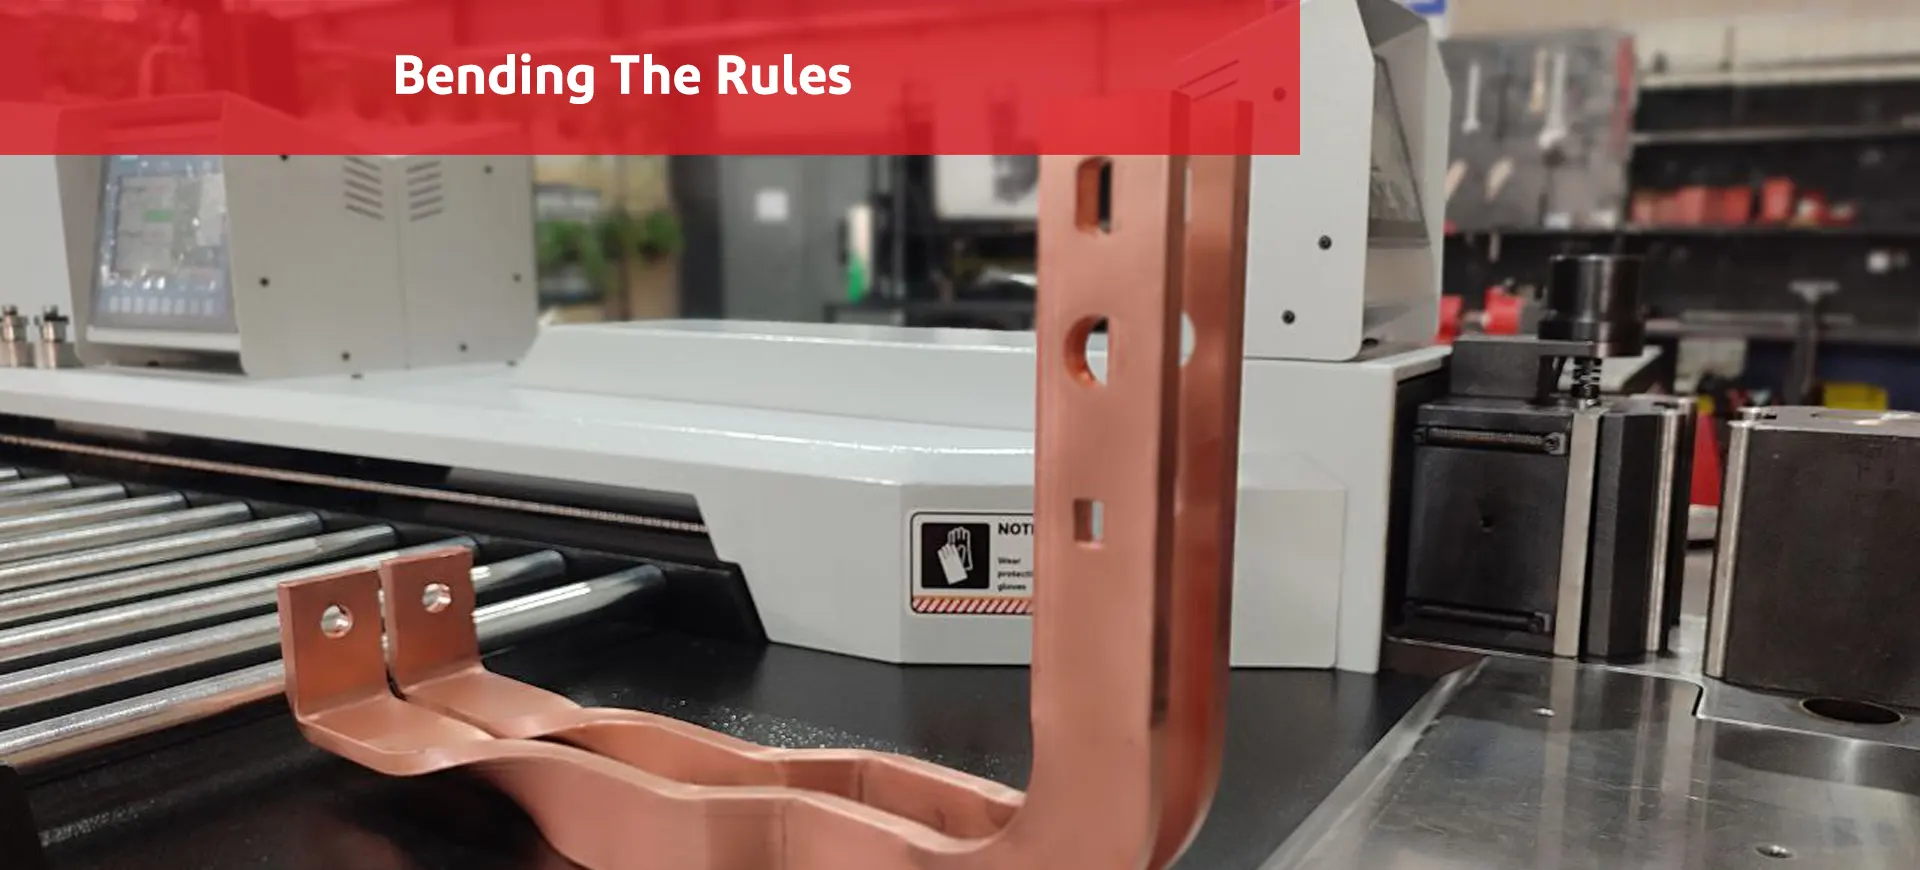
Busbar bending is the cold forming of a flat copper or aluminum conductor to a specified angle, radius and position so that it connects breakers, terminals and other busbars without strain. Because busbars carry high currents in a compact space, every bend has to hold its dimensions: a bar that is a few degrees off will not line up with its bolt holes, and installers end up pulling it into place. That built-in stress loads the bolted joint instead of leaving it to carry current only. Low-voltage assemblies are designed and verified against the IEC 61439-1 assembly rules, so consistent busbar geometry is part of building a compliant panel.
Types of Busbar Bends: Flat, Edge, Twist and Offset
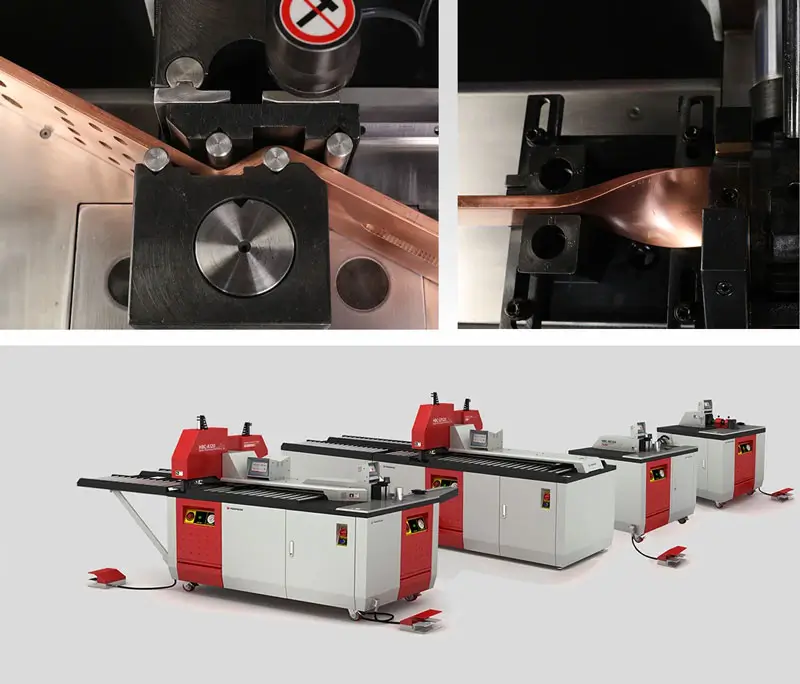
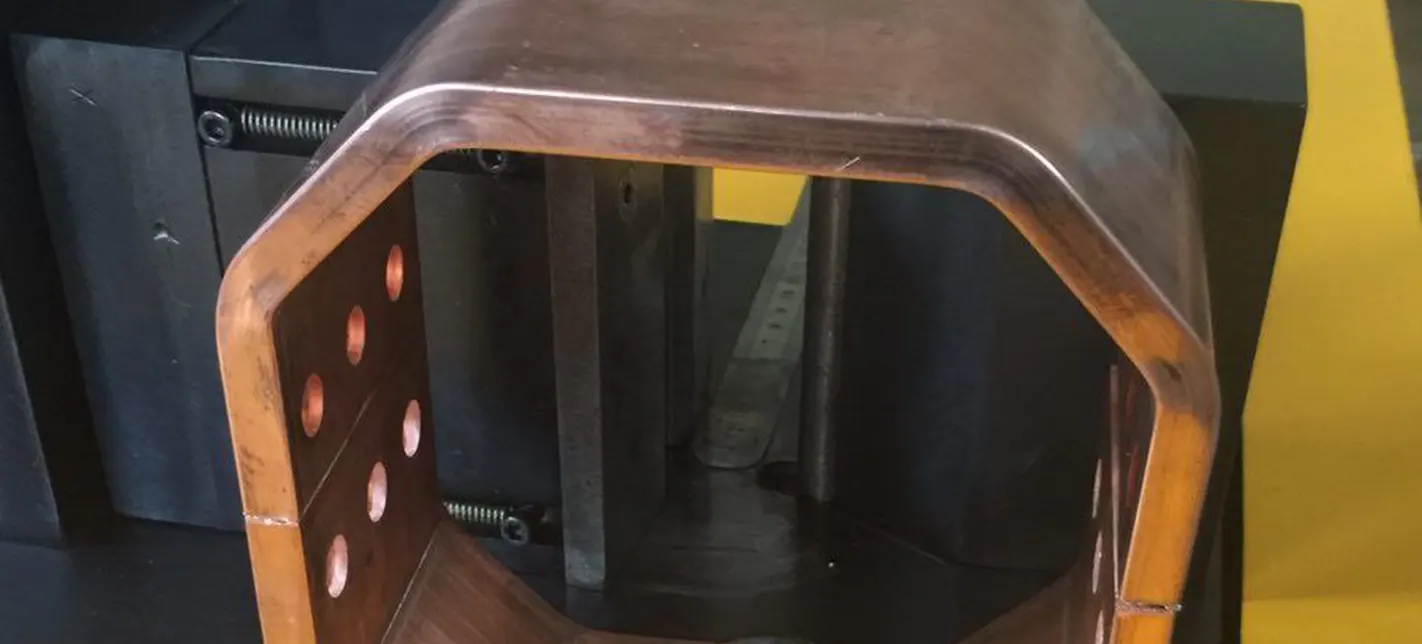
Most busbar layouts are built from four basic bends: flat bends, edge bends, twists and offsets. Fabricators often call bent bars folded bus bars, because each bend folds the strip into a new plane or direction. The bend type determines the tooling and force required, and edge bends in particular need far more force than flat bends because the bar is bent across its width. Every bend also springs back slightly when the load is released, which is why tooling is set to overbend; springback is the material’s attempt to return to its original flat position, as The Fabricator’s springback article explains.
| Bend type | What happens to the bar | Typical use |
|---|---|---|
| Flat bend (flat-wise) | Bent across its thickness, around the narrow face | Changing level between breaker rows or panel sections |
| Edge bend (edge-wise) | Bent across its width, in its own plane | Turning a run 90° without changing its plane |
| Twist | Rotated about its long axis, usually 90° | Matching a terminal that faces a different direction |
| Offset (double bend) | Two opposite flat bends close together | Stepping around another bar or support |
Bus Bar Bending Methods Compared: Manual, Hydraulic, CNC and 3-in-1
Bus bar bending is done with four main methods: manual benders, hydraulic benders, CNC bending machines and 3-in-1 machines that also cut and punch. The right choice depends on bar size, bend complexity and how many identical parts you produce. A hydraulic busbar bender covers most panel-shop work, while CNC control pays off when the same bend program repeats across large batches. Whatever the method, the bend must leave contact areas flat and undamaged, because joint performance is a design topic of its own in the CDA Copper for Busbars guide.
| Method | Angle repeatability | Bar size range | Best fit |
|---|---|---|---|
| Manual bender | Depends on operator | Small and thin bars | Site work, repairs, one-off parts |
| Hydraulic bender | Good with angle stop or gauge | Medium to thick bars | Panel shops, mixed production |
| CNC bending machine | High, program-controlled | Medium to thick bars | Repeat batches, complex multi-bend parts |
| 3-in-1 machine | Good with angle stop or gauge | Within the machine’s rated capacity | Workshops that cut, punch and bend at one station |
Manual Busbar Bending
Manual busbar bending is a traditional method that involves using hand tools or manual bending machines to shape busbars. While it may not offer the precision or efficiency of automated techniques, manual bending is still widely used, especially in smaller-scale projects or when working with limited budgets.
Advantages of Manual Bending:
- Cost-Effective: Manual bending equipment is generally less expensive than automated machinery, making it accessible for small workshops or individual projects.
- Flexibility: Manual bending allows for greater control and adaptability, enabling engineers to make adjustments on the fly.
- Simplicity: The straightforward nature of manual bending means that it requires less training and technical expertise.
Considerations:
- Precision: Manual bending may not achieve the same level of precision as automated methods, potentially leading to inconsistencies in bend angles and radii.
- Labor-Intensive: The process can be time-consuming and physically demanding, particularly when working with thicker or harder materials.
Hydraulic Busbar Bending
Hydraulic busbar bending machines use a hydraulic cylinder to push the bar into a die, giving controlled, high force for bending busbar in copper or aluminum across a wide range of widths and thicknesses. An angle stop or digital angle gauge sets where the ram stops, so identical bends can be repeated across a batch without re-marking each bar. This makes hydraulic bending the standard choice for medium and large panel production. The press works on Pascal’s principle, where a larger piston area produces a correspondingly larger force, as the hydraulic press article on Wikipedia explains.
Advantages of Hydraulic Bending
– Precision and Consistency: Hydraulic busbar bender machines provide accurate and repeatable bends, ensuring uniformity across multiple busbars.
– Power and Versatility: The hydraulic system allows for the bending of thicker and harder materials that would be challenging to bend manually.
– Efficiency: Hydraulic bending is faster than manual methods, increasing productivity in high-volume manufacturing settings.
Considerations:
- Cost: Hydraulic machines can be a significant investment, requiring a higher initial outlay than manual tools.
- Maintenance: Regular maintenance is necessary to keep hydraulic systems functioning smoothly, adding to operational costs.
CNC Busbar Bending
CNC busbar bending uses a programmable controller to set the bend angle, bend position and, on some machines, the backgauge for every bend in a part. The operator enters or loads a bend program once, and the machine repeats it for each bar in the batch, which reduces measuring, marking and operator-dependent variation on multi-bend parts. CNC bending is most cost-effective for repeat orders, standardized panel designs and parts with several bends in sequence. Computer numerical control is the automated control of machine tools by a computer, and closed-loop control provides the repeatability metalworking machines require, according to the Wikipedia overview of CNC.
Advantages of CNC Bending
- Repeatability: Stored programs produce the same angles and positions across batches.
- Complex parts: Multi-bend parts are produced in sequence without re-measuring between bends.
- Less operator dependence: Results rely less on individual skill once the program is proven.
Considerations
- Investment: CNC machines cost more than manual or standard hydraulic benders.
- Programming time: Short runs of one-off parts may not justify the setup time.
3-in-1 Busbar Machines
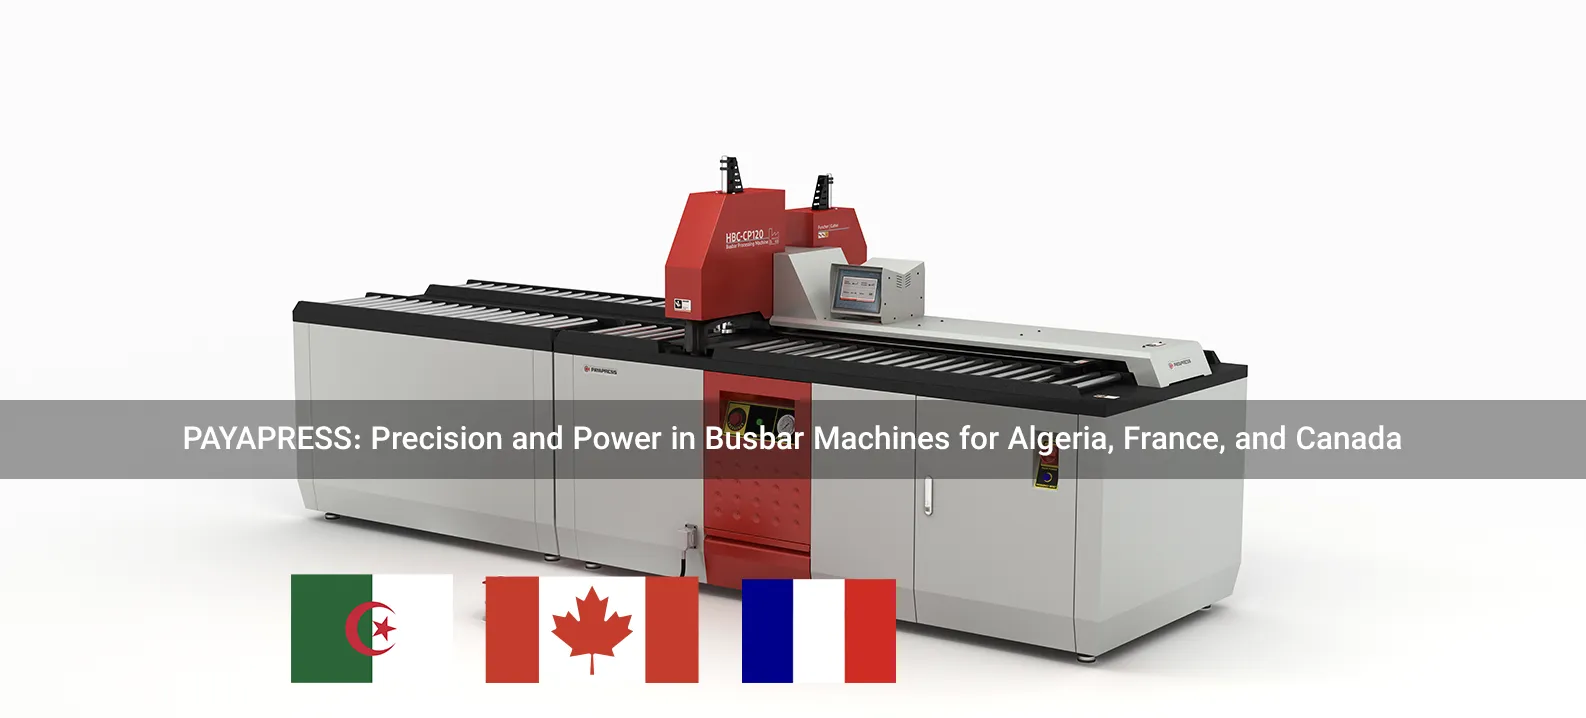
3-in-1 busbar machines combine cutting, punching and bending stations in one machine, so a bar can be cut to length, punched for its bolt holes and bent without moving to separate equipment. This saves floor space and handling time, which suits workshops that produce a wide mix of busbar parts in moderate volumes. Machine choice should start from the largest bar you need to process. Bar width and thickness follow from the required current rating, as shown in the CDA copper busbar ampacity data.

Advantages of 3-in-1 Machines
- Complexity: Three stations on one machine mean more tooling and setup options to learn, so plan operator training for each station before full production.
- Capacity: Each station has its own maximum bar size, and the bending station usually sets the limit. PAYAPRESS 3-in-1 machines come in 120, 160 and 200 series [VERIFY: maximum bar size per 3-in-1 model]; for reference, the dedicated HBC-BE bending series is rated at 120 × 12 mm, 160 × 15 mm and 200 × 20 mm.
Considerations:
– Complexity: While operating a 3-in-1 machine may seem complex, PAYAPRESS machines are designed with user-friendliness in mind. Intuitive controls and clear instructions make learning to use these machines a breeze, eliminating the need for extensive training.
– Capacity: PAYAPRESS 3-in-1 machines offer impressive capacity. Our 120 series can easily process up to 120*12mm busbars, while the 160 series can handle 160*15mm. For larger requirements, we can customize our machines to process up to 200*20mm busbars.
How to Choose a Busbar Bending Technique
Material and thickness decide how much force a bend needs and how tight it can be. Copper is the most common busbar material and bends predictably when annealed, while aluminum needs a larger cross-section for the same current, so aluminum bars are usually wider or thicker for the same rating. Thicker and wider bars call for hydraulic or CNC machines, and copper-specific techniques are covered in our guide to copper busbar bending. An aluminum busbar needs roughly 1.6 times the cross-sectional area of a copper equivalent, according to this aluminum vs copper busbar comparison.
Material and Thickness
The material and thickness of the busbar play a crucial role in determining the appropriate bending technique. Copper and aluminum are the most commonly used materials, each with unique properties that affect their bendability. Thicker busbars may require more powerful machines, such as hydraulic, to achieve precise bends without damaging the material.
Bend Radius and Angle
The desired bend radius and angle are important considerations when choosing a bending technique. Tight radii or complex bend profiles may necessitate the use of hydraulic busbar bending machines, which offer the precision and control needed to execute intricate bends accurately.
Production Volume
The scale of the project and production volume will influence the choice of bending technique. For high-volume manufacturing, automated methods like hydraulic bending are preferred due to their speed and efficiency. In contrast, manual bending may be more suitable for smaller-scale operations or custom projects with lower production demands.
Budget and Resources
Budget constraints and available resources are critical factors in determining the most appropriate bending technique. While CNC machines offer the highest precision, they also come with a higher price tag. For businesses with limited budgets, hydraulic bending may provide a more cost-effective solution.
Quality Checks for Precision Bent Copper Busbar Parts
Precision bent copper busbar parts are judged on four things: bend angle, the position of each bend relative to the holes, flatness of the contact areas, and a clean, undamaged surface. If any of these drifts, the part will not fit the panel without force, or its bolted joints will not seat flat. Checking the first part of each batch against the drawing catches setup errors before a whole batch is bent. Each of these dimensions should carry a tolerance on the drawing, meaning the permissible limit of variation, as defined in the engineering tolerance overview.
| Check | What to measure | Why it matters |
|---|---|---|
| Bend angle | Angle after springback, with a protractor or angle gauge | Wrong angles shift every downstream hole |
| Bend position | Distance from bar end or hole to the bend line | Holes must line up with terminals and other bars |
| Contact flatness | Flatness of joint areas near the bend | Bolted joints need full, flat contact |
| Surface condition | Tool marks, cracks on the outer radius, plating damage | Damage reduces contact quality and corrosion protection |
Applications of Busbar Bending
Busbar bending is an essential process in various industries and applications, where precise and reliable power distribution is crucial. Some of the most common applications include:
Power Distribution Systems
Busbars are integral components of power distribution systems, where they facilitate the efficient transmission of electricity from power sources to end-users. Properly bent busbars ensure seamless integration within switchgear and distribution panels, minimizing energy loss and enhancing system reliability.
Transformers
In transformers, busbars are used to connect winding terminations and facilitate the flow of electricity between the primary and secondary coils. Accurate busbar bends are essential for maintaining the integrity of these connections and ensuring optimal transformer performance.
Electrical Panels
Electrical panels, including control panels and distribution boards, rely on busbars to organize and distribute electrical power. Properly bent busbars allow for efficient use of space within panels, ensuring that electrical components are neatly and securely connected.
Renewable Energy Systems
In renewable energy systems, such as solar and wind installations, busbars play a vital role in connecting power generation equipment to the grid or storage systems. Precise busbar bending ensures that these connections are reliable and efficient, maximizing the overall performance of the renewable energy system.
Conclusion: Matching the Busbar Bending Method to the Job
Busbar bending comes down to producing the right bend type at the right angle and position, every time. Manual benders suit small jobs and site work, hydraulic machines cover most panel production, CNC machines pay off on repeat multi-bend parts, and 3-in-1 machines save space where cutting, punching and bending share one station. Start from your largest bar size, your bend types and your batch volume, then choose the method that holds your tolerances at that volume.


Rate this article
Choose a rating from 1 to 5 stars.
No ratings yet
0 Comments
No comments yet. Be the first to comment.